About Carbon Black
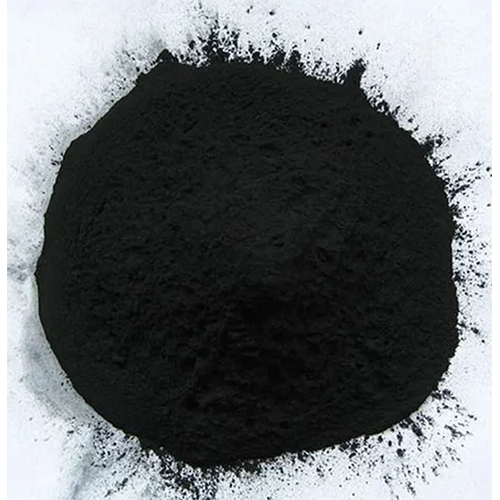
Discover the must-have Carbon Black-a sensational industrial masterpiece, coveted by manufacturers and laboratories alike. With a majestic particle size range (10-500 nm), superior surface area (up to 1500 m2/g), and high conductivity, this pigment stands out across a plethora of uses. Its color index number 77266 guarantees ultradeep black, perfect for pigments, inks, rubber reinforcement, plastics, and conductive agents. Virtually indefinite shelf life and non-toxic classification make this powder reliable and versatile. Find your last chance to elevate your products with this high-purity, stable material-crafted for exceptional results.
Advanced Features and Application Insights
Carbon Black boasts extra features such as oil absorption (1.5-4.0 ml/g) and stability under recommended conditions. Widely used by industrial manufacturers, researchers, and laboratories, it's ideal for pigmenting, enhancing rubber strength, and serving as a conductive agent. To apply, simply blend into target compounds or suspensions. Its amorphous, fine powder form allows seamless integration with inks, paints, plastics, cables, and batteries, becoming indispensable in innovative and demanding environments.
Efficient Delivery, Sample Policy, and Export Markets
Experience prompt dispatching and secure shipping for Carbon Black across major export markets, including Asia and Europe. Samples can be provided to ensure suitability for your outlay, promoting satisfaction before bulk orders. Our delivery partners adhere to stringent handling protocols, ensuring the powder's integrity upon arrival. Orders are processed swiftly, minimizing lead time and maximizing productivity for commercial, industrial, or laboratory needs-guaranteeing your last chance at premium quality material reaches you rapidly and safely.
FAQ's of Carbon Black:
Q: How should Carbon Black be stored to maintain optimal quality?
A: Carbon Black should be stored in a cool, dry area away from ignition sources. Proper storage conditions help preserve its stability and virtually indefinite shelf life.
Q: What is the recommended application method for Carbon Black in industrial settings?
A: It is typically integrated into mixtures or suspensions with pigments, rubber, inks, plastics, or coatings, ensuring uniform dispersion for optimal performance in end products.
Q: Where can Carbon Black be used to achieve high conductivity?
A: This material is suitable for conductive agents in batteries, cables, coatings, and electronics applications, owing to its high conductivity characteristics.
Q: When can I expect dispatching and delivery after placing an order?
A: Orders are dispatched promptly after confirmation, with secure shipping processes in place to minimize transit time and guarantee timely delivery.
Q: What are the main benefits of using Carbon Black in manufacturing?
A: Manufacturers gain from its superior pigmenting strength, reinforcement properties in rubber, stability, non-toxicity, and remarkable conductivity, enhancing overall product durability and quality.
Q: Is there a sample policy available for Carbon Black purchases?
A: Yes, samples are available upon request, allowing customers to evaluate the product before committing to larger orders.





 Send Inquiry


 Send Inquiry
